SOURCING & BUDGETING GUIDE
Optical Lens Injection Molding Cost: How Tooling and Unit Prices Are Actually Calculated
An engineering framework for custom plastic optics procurement—learn what drives NRE tooling costs and per-part unit prices, so you can evaluate supplier RFQs based on actual manufacturing requirements.
By: ATRMOLD Engineering Team
Sep 2026
Reading time: 12min
Category: Sourcing & Program Planning
- Why Custom Optical Lens Injection Molding Cost Requires Engineering Context
- The Two Cost Buckets: NRE Tooling vs. Per-Part Unit Price
- Primary Cost Drivers in Optical Mold Tooling (NRE)
- Key Variables Influencing Per-Part Unit Price at Scale
- How Sub-Micron Optical Tolerances Elevate Costs Beyond Standard Injection Molding
- The Amortization Curve: Evaluating Tooling Costs Across Production Volumes
- Hidden Overhead Factors in Custom Optical Lens Sourcing
- How to Conduct an Apples-to-Apples RFQ Quote Comparison Incomplete / Ambiguous RFQ Quote
- Optical Lens Sourcing Checklist for Procurement Engineers
- Frequently Asked Questions (FAQ)
Asking “How much does an optical lens cost?” rarely yields a simple, fixed answer. Any custom plastic optics supplier providing a flat pricing sheet without first evaluating design geometry, resin specifications, tight-tolerance requirements, and annual volume is oversimplifying the manufacturing requirements of optical molding. Rather than serving as a standard price catalog, this guide explains the financial and technical mechanics governing optical lens injection molding cost structures. By understanding how non-recurring engineering (NRE) tooling expenses and piece prices interact, procurement managers and hardware design engineers can evaluate supplier quotes objectively based on real manufacturing parameters.
Because pricing varies with raw polymer markets, global supply chains, and component specifications, publishing fixed unit costs is impractical. Instead, we break down the engineering logic behind custom optical lens manufacturing budgets so you can analyze supplier RFQ line items with clarity.
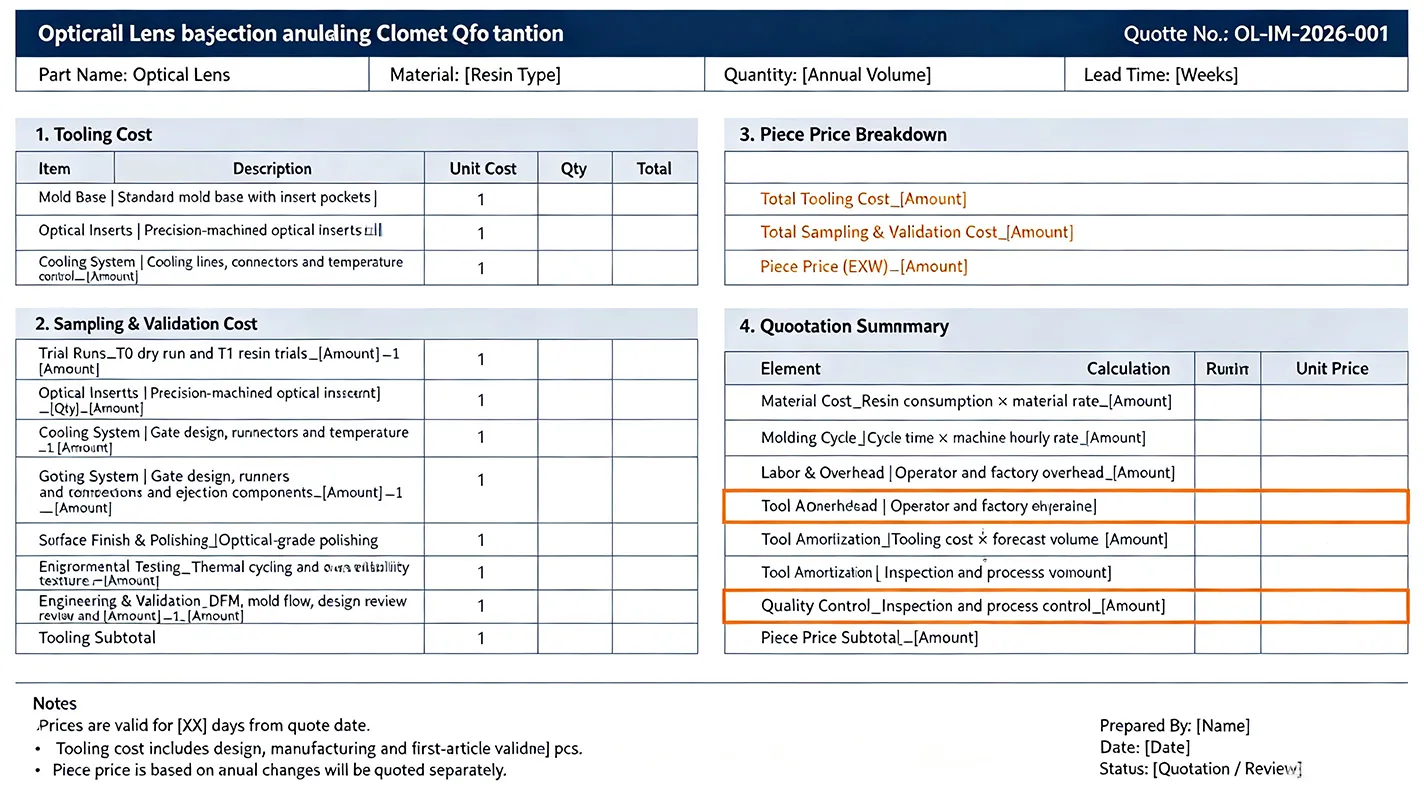
1. Why Custom Optical Lens Injection Molding Cost Requires Engineering Context
A comprehensive cost estimate for precision plastic optics involves four key variables: amortized mold tooling investment, resin cost per unit, machine processing time, and post-molding secondary operations. For precision optics, tight surface-finish requirements, wavefront error limits, and optical coating processes can affect each phase of production. Consequently, two optical components with identical outer dimensions can vary significantly in cost depending on surface-figure specifications, core-insert polishing requirements, and cleanroom quality-control standards.
2. The Two Cost Buckets: NRE Tooling vs. Per-Part Unit Price
Every professional optical injection molding quote splits into two primary financial categories:
NRE Tooling Cost
One-time capital expenditure for mold design, machining, and insert polishing
Per-Part Unit Price
Recurring piece price driven by polymer grade, press time, and yield rate
NRE (Non-Recurring Engineering) tooling costs cover mold design and fabrication—an upfront investment that can be amortized over the total lifecycle volume. The per-part unit price reflects ongoing production expenses, including optical polymer resins, injection molding machine time, cleanroom labor, and optical metrology. Balancing these two components is essential for optimizing overall project expenditures across various production tiers.
3. Primary Cost Drivers in Optical Mold Tooling (NRE)
Fabricating a high-precision optical injection mold requires specialized toolmaking techniques that can significantly increase costs compared with standard plastic housing molds:
Mold Cavity Count: Scaling from a single-cavity prototype tool to a multi-cavity production mold can increase tooling cost by 1.5× to 2.5. However, multi-cavity tools multiply part output per press cycle, lowering long-term piece price.
Tool Steel Selection & Hardness: High-grade stainless mold steels, such as Stavax ESR, offer corrosion resistance and good polishability for long production runs, although they require a higher upfront investment in material and machining.
SPDT Core Insert Machining: Machining spherical, aspheric, or freeform optical surfaces may require Single-Point Diamond Turning (SPDT) to achieve the required form accuracy and surface finish, adding specialized labor and machine time.
Complex Mechanics & Side-Actions: Integrating mechanical lifters, side-pull slides, or complex parting line shut-offs increases tool build complexity and machining costs.
Precision Tooling Tolerances: Maintaining ultra-tight tool tolerances can require extended Wire EDM, CNC EDM, and hand-polishing cycles before the first molding trial.
4. Key Variables Influencing Per-Part Unit Price at Scale
Once an optical mold is qualified, the recurring unit price is shaped primarily by processing parameters and yield management:
Injection Press Cycle Time: Thicker optical elements often require longer cooling and packing cycles to control internal stress, sink marks, and void-related defects. Because machine rate is billed per hour, cycle time directly impacts per-part costs.
Optical Resin Selection: Specialty polymers—such as optical PMMA, optical PC, or Cyclic Olefin Polymers (COC/COP like Zeonex or Topas)—differ in cost. High-performance COP resins, which generally offer low moisture absorption and low birefringence, can carry higher raw material costs per kilogram than standard acrylics.
Process Yield & Scrap Rates: Microscopic dust inclusions, surface haze, or internal stress can render an optical component unusable. Higher aesthetic and functional inspection standards reduce net yields, shifting scrap costs onto the final piece price.
Secondary & Finishing Operations: Anti-reflective (AR) coatings, hardcoating, dip coating, ultrasonic cleaning, and automated optical inspection (AOI), where required, add per-unit costs to the molded optic.
5. How Sub-Micron Optical Tolerances Elevate Costs Beyond Standard Injection Molding
A standard industrial plastic housing and a precision custom optical lens may share similar dimensions, yet their manufacturing economics differ substantially. Optical components may require tight surface-figure accuracy, controlled birefringence, strict transmittance requirements, and controlled chromatic aberration. Achieving these requirements demands specialized molding machinery, environmental cleanroom controls (Class 10,000 / ISO 7), and advanced metrology setups—including interferometers, spectrophotometers, and MTF (Modulation Transfer Function) testers. Detailed quality procedures are covered in our optical lens quality control and metrology guide.
Procurement Insight: Quotes offering unusually low unit prices may exclude necessary cleanroom controls, optical metrology, or yield allowances. Unfunded quality controls in initial estimates often re-emerge later as yield drop-offs or unquoted secondary testing fees.
6. The Amortization Curve: Evaluating Tooling Costs Across Production Volumes
NRE tooling costs can dominate total program budgets at low volumes (e.g., 1,000 to 5,000 units). As production scales into tens or hundreds of thousands of units, fixed tooling costs amortize down to a fraction of the total budget, leaving polymer material and injection molding press rates as the primary cost drivers. Selecting an optimal tooling strategy depends on product lifecycle forecasts: investing in a higher-cavity, hardened-steel mold can reduce total cost per part over extended high-volume runs.
Strategic Recommendation: Always request multi-tiered RFQ quotes (e.g., 5,000, 25,000, 100,000, and 500,000 units/year). Evaluating piece price variations across volume steps prevents premature commitment to under-powered prototype molds or over-engineered production tooling.
| Overhead Factor | Why It Is Often Omitted in Initial Quotes |
|---|---|
| Optical Performance Validation | Precision optical metrology (MTF testing, spectrophotometry, wave-front analysis) is often billed separately unless explicitly scoped into the initial RFQ. |
| Post-Molding Stress Relief (Annealing) | Thermal baking or annealing cycles, when required to reduce residual stress and birefringence, are sometimes omitted from standard plastic processing quotes. |
| Cleanroom Anti-Static Packaging | Custom thermoformed trays and vacuum-sealed anti-static bags necessary to prevent surface scratches are occasionally overlooked in basic packaging budgets. |
| Steel-Safe Tooling Corrections | Modifying core optical inserts post-T1 trial to achieve exact focal length targets adds turnaround time and rework labor. |
| Preventative Tool Maintenance | High-volume production may require periodic disassembly, cleaning, and insert re-polishing to preserve surface-finish quality throughout the tool’s service life. |
8. How to Conduct an Apples-to-Apples RFQ Quote Comparison
Incomplete / Ambiguous RFQ Quote
- Blended lump sum without distinguishing NRE tooling costs from recurring unit prices
- Omitted tooling details (cavity count, steel grade, expected mold life)
- Unclear inspection criteria, cleanroom class, or metrology scope
- Single-volume pricing model without scale-up tiers
Comprehensive / Transparent Engineering Quote
- Itemized breakdown separating NRE tooling, resin costs, and processing fees
- Clear mold specifications (e.g., steel grade, SPDT inserts, and cavity count)
- Clearly defined optical quality standards, yield assumptions, and metrology requirements
- Structured unit price tiers across multiple annual production volumes
Related Engineering Resources
9. Optical Lens Sourcing Checklist for Procurement Engineers
Does the quote explicitly break down NRE tooling costs, resin costs, processing time, and secondary finishing charges?
What specific tool steel, cavity count, and core insert manufacturing method (e.g., SPDT) are specified?
Are optical metrology requirements (transmittance testing, wavefront error, MTF, and Cpk reporting) included in the unit price?
Is the piece price quoted across multiple annual volume tiers (e.g., 10k, 50k, 250k units)?
What estimated scrap rate and process yield percentage are factored into the unit cost model?
Is cleanroom-compatible anti-static tray packaging included to prevent surface damage during transit?
Frequently Asked Questions (FAQ)
Why do custom optics manufacturers avoid providing immediate unit pricing without 3D CAD files?
Precision optics pricing depends heavily on lens geometry, wall thickness, surface curvature, polymer selection, and tight-tolerance requirements. Without detailed 3D CAD models and 2D engineering drawings, it can be difficult to accurately predict press cycle times, tooling complexity, and yield rates.
When is a multi-cavity optical mold financially justified?
Multi-cavity tools carry higher upfront NRE tooling costs (typically 1.5× to 2.5× those of a single-cavity design) but can reduce machine time per part. Multi-cavity molds are generally economical when annual volume demands offset initial tooling expenditures through reduced press time per unit.
How do optical tolerances impact manufacturing costs compared to standard plastic parts?
Tight optical surface-figure requirements, focal-length tolerances, and low birefringence can require Single-Point Diamond Turning (SPDT), mirror-finish cavity polishing, specialized injection or injection-compression molding equipment where required, cleanroom operations, and dedicated interferometric metrology—all of which can increase baseline tooling and unit costs.
What hidden line items commonly cause budget overruns in optical lens molding?
Omitted post-molding processes such as thermal annealing, unbudgeted secondary optical coatings (AR/hardcoat), custom anti-static tray packaging, and unpriced metrology validation (such as MTF and spectral transmittance testing) can be common sources of unexpected expenses.
How should hardware engineering teams evaluate tooling costs vs. unit price trade-offs?
Evaluate total program expenditure over the expected product lifespan. Calculate total cost using the formula: Total Cost = NRE Tooling Cost + (Unit Price × Lifecycle Volume). Comparing options across multiple production tiers helps identify the most cost-effective tooling strategy for your target volume.
Calculating optical lens injection molding costs requires analyzing upfront NRE tooling investments alongside recurring per-part production expenses. By evaluating resin properties, cycle times, sub-micron tolerances, and quality control requirements, procurement teams can review supplier quotes objectively and prevent unexpected cost overruns. If you are preparing a budget for a custom plastic optics program, use the checklist in Section 9 to align technical expectations with your manufacturing partner.
Budgeting a Custom Optical Lens Program?
Connect with our optics engineering team for a detailed cost breakdown based on your 3D CAD models, target optical specifications, and volume requirements.
ATRMOLD — Precision Optical Lens Injection Molding & Mold Manufacturing